01 · Integrally bladed rotor
Blisk machining
Blades and disk machined from one forging. 5-axis roughing, blade and hub finishing, edge and fillet control.
Simultaneous 5-axisInconel · titaniumKitamura HX500
Houston, TX · ISO 9001 & AS9100D compliant
We machine blisks, blings, inducers, turbine impellers and turbine blades from Inconel, titanium and stainless steel on simultaneous 5-axis and 9-axis CNC machines. Houston, Texas, serving engineers and buyers across the U.S.
Not every CNC machine shop is crafted equal. Ours is set up for bladed parts, hard alloys and one-setup work.
Bladed rotating parts are some of the hardest work in machining. They have thin airfoils, tight blade-to-blade spacing, compound curves and expensive alloys. That is the work we set up for: 5-axis toolpaths in ESPRIT EDGE, rigid horizontal machining, and a team that reads the print before quoting it.
Blades and disk machined from one forging. 5-axis roughing, blade and hub finishing, edge and fillet control.
Ring-mounted blade rows for compressor and turbine stages. Thin-section workholding and controlled stock removal.
Helical inducer vanes with long, wrapped blades. Machined complete on 5-axis or 9-axis mill-turn.
Open and shrouded-style impellers with splitter blades. Hub, blade and fillet finishing in one setup where possible.
Rotor blades and vanes with root forms. Airfoil, platform and root machined to the model.
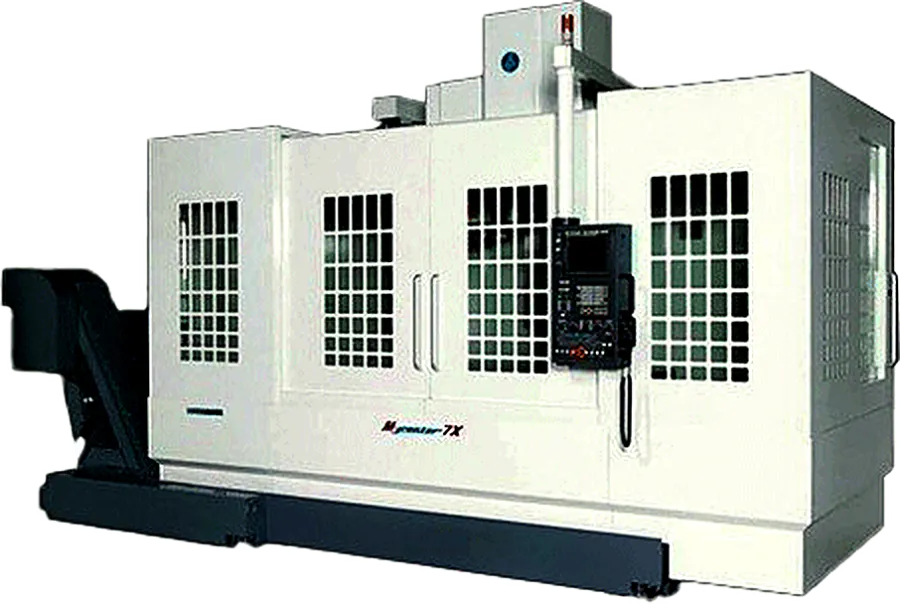
Long shafts, big-bore turned parts and large milled plates. 60.2 in X travel and 62.9 in turning length.
Rigid horizontal 5-axis, mill-turn with a B-axis head, and a part envelope sized for real turbomachinery hardware.
Six things that decide whether a bladed part comes off the machine right the first time.
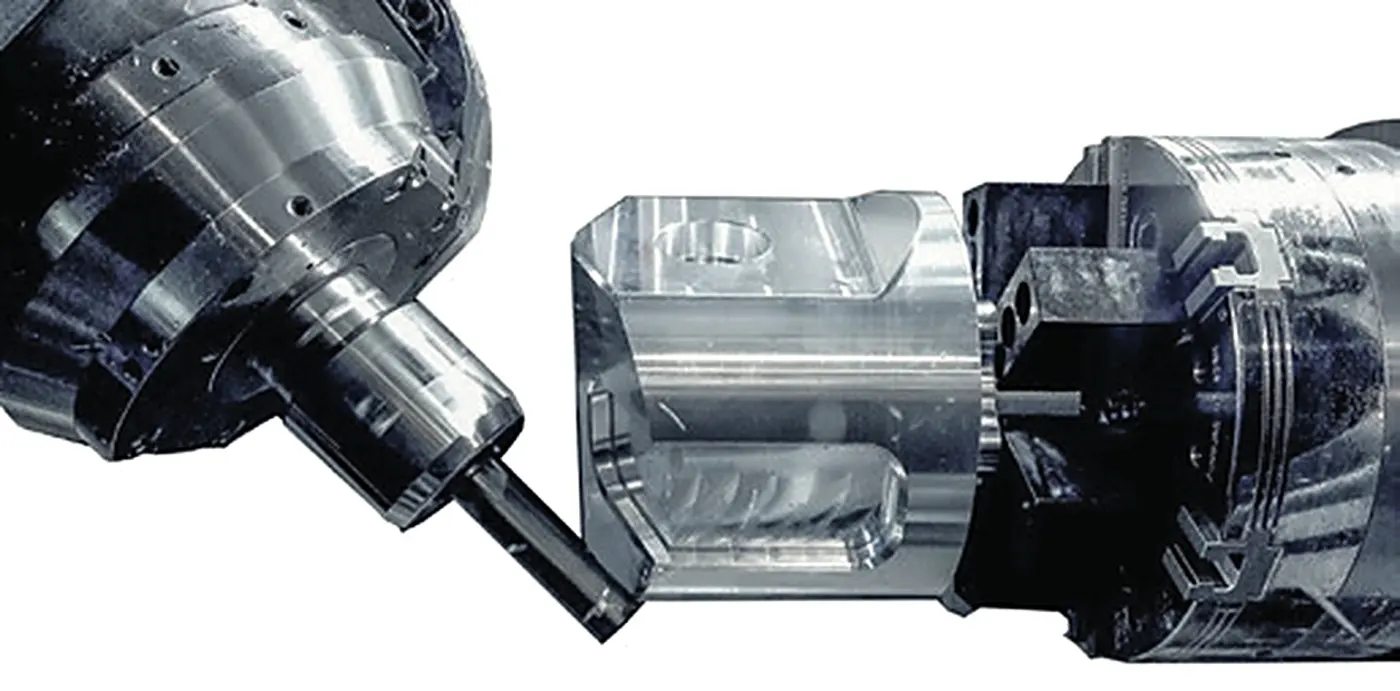
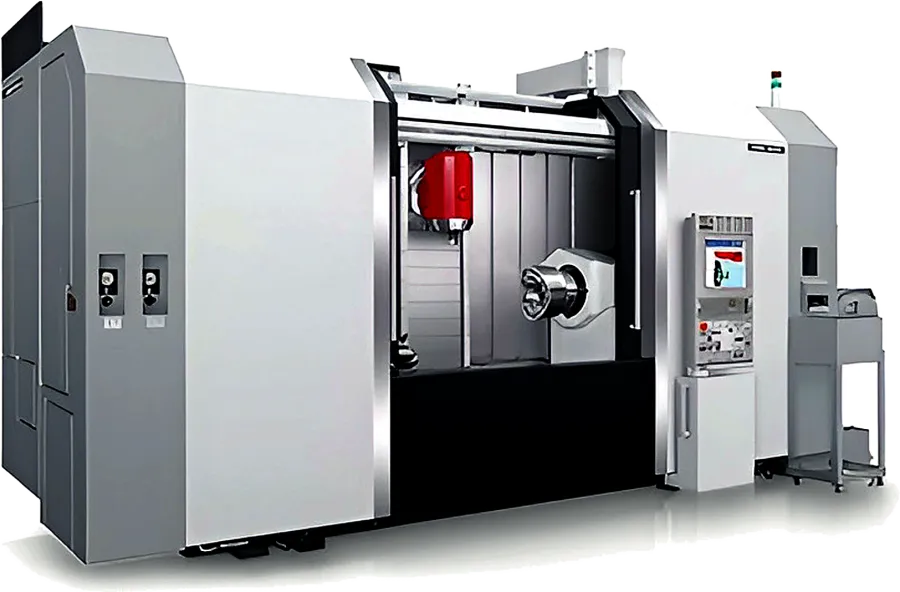
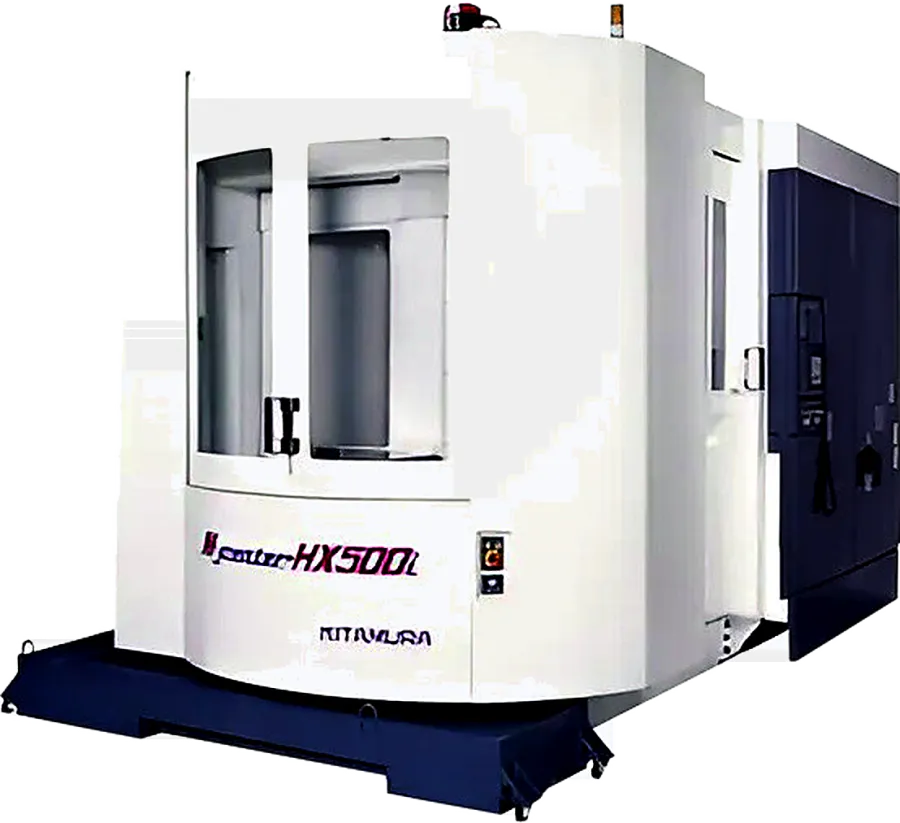
On a Kitamura HX500 horizontal machining center. A horizontal spindle clears chips well when machining deep blade passages.
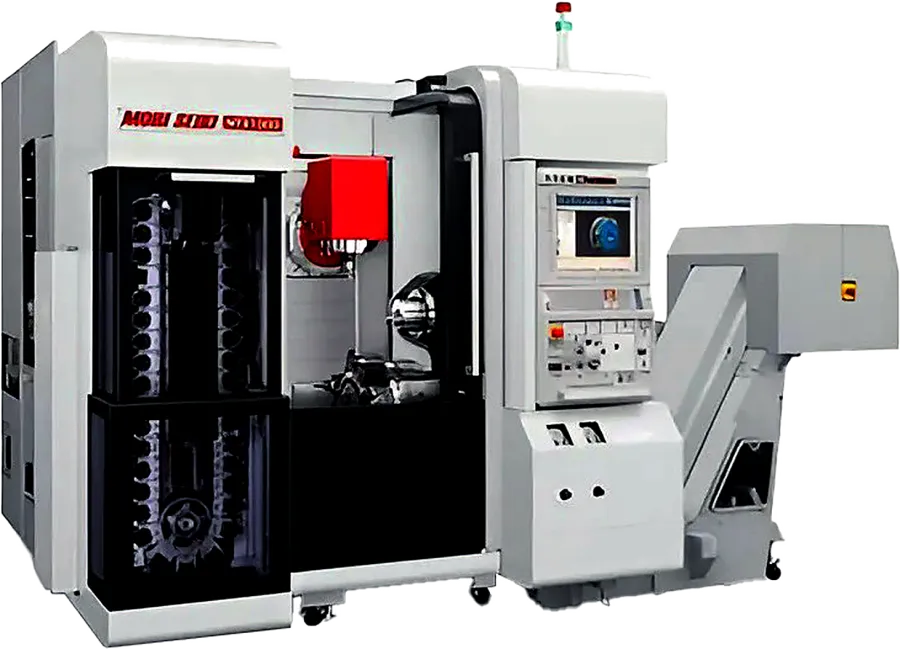
Mori Seiki NT-series machines with a B-axis milling head and sub-spindle. Turned and milled features in one setup, without re-fixturing errors.
Dedicated impeller and blisk strategies for roughing, blade finishing, hub floors and fillets, checked in full machine simulation.
Nickel, cobalt and titanium alloys:
A KUKA robot keeps repeat production running unattended, so it stays consistent and costs less.
Tracked in our own digital shop-floor system. How it works
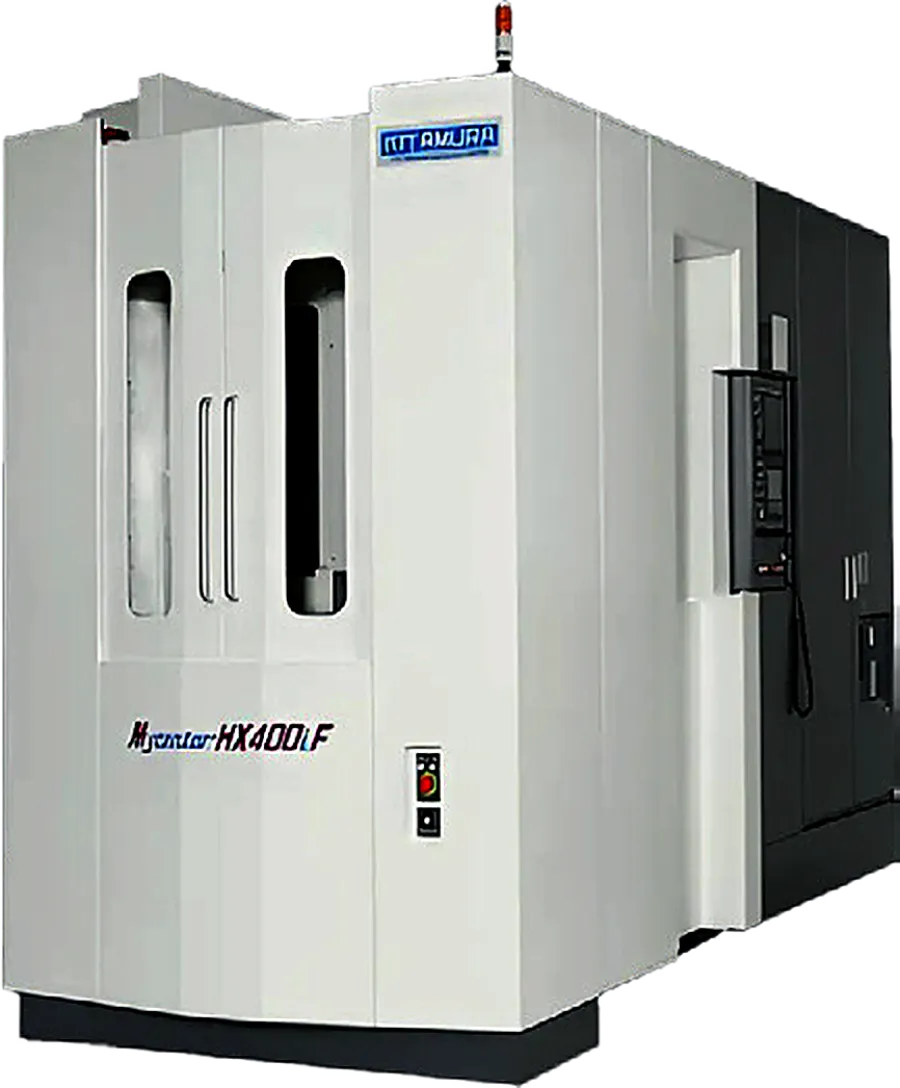
Pick a machine to see its envelope and what we use it for. Full equipment list.
We also make our established product lines: titanium high-temperature flanges, pipeline fittings, power-plant boiler components and welded carbon-steel reducers and elbows.
A person on our team reads every RFQ. If something on the print will drive cost or risk, we tell you before you order.
Drawing, STEP model, quantity, material and required date.
Geometry, material and tolerances, by hand. Questions come back early.
Written price and lead time, every time.
We machine blisks (integrally bladed rotors), blings (bladed rings), inducers, turbine and compressor impellers, and turbine rotor blades to customer prints. Work runs on our Kitamura HX500 simultaneous 5-axis machining center and our Mori Seiki 9-axis mill-turn centers, programmed in ESPRIT EDGE.
Our shop is in Houston, Texas. We quote and ship to customers across the United States.
More than 100 superalloy grades, including Inconel 600 to 939, Waspaloy, Udimet, Hastelloy C-276, C-22 and X, Haynes 230 and 282, Nimonic, René 41 to 104, Incoloy, MAR-M 247, CMSX-4, A-286 and Stellite; titanium Grade 5 (Ti-6Al-4V) and Grade 2; 17-4 PH, 13-8 and 316L stainless; duplex; Monel; and 6061/7075 aluminum. If your alloy is not listed, send the print and we will tell you straight whether it is a fit.
Our 5-axis envelope is Ø31.5 in × 43.5 in high on the Kitamura HX500. Turned parts can be up to Ø26 in and 62.9 in of turning length on the Mori Seiki NT4200. Our vertical machining center travels 60.2 in in X. Our maximum part length is 82 in.
Our quality system is compliant with ISO 9001:2015 and AS9100D, with full material traceability, first article inspection and a certificate of conformance on every shipment. Third-party certification is planned.
Yes. We manufacture steam and gas turbine rotor blades, compressor blades and stator vanes to print, 5-axis machining the airfoil, platform and dovetail or fir-tree root from bar, forgings or blanks, with heat-lot traceability on every blade.
Yes. We TIG weld and machine as one job, mainly carbon steel reducers, elbows, pipeline fittings and fabricated housings, with finish machining after welding.
Use the request-a-quote form or email your drawing and STEP model to info@jepmfg.com. Include quantity, material and your required date. Every quote includes a lead time.
Send it over. We review every RFQ by hand and include a lead time with every quote.